Tungsten Points for X10 3.2mm Parallel Pro & Revelation
Tungsten Points for X10 3.2mm Parallel Pro & Revelation
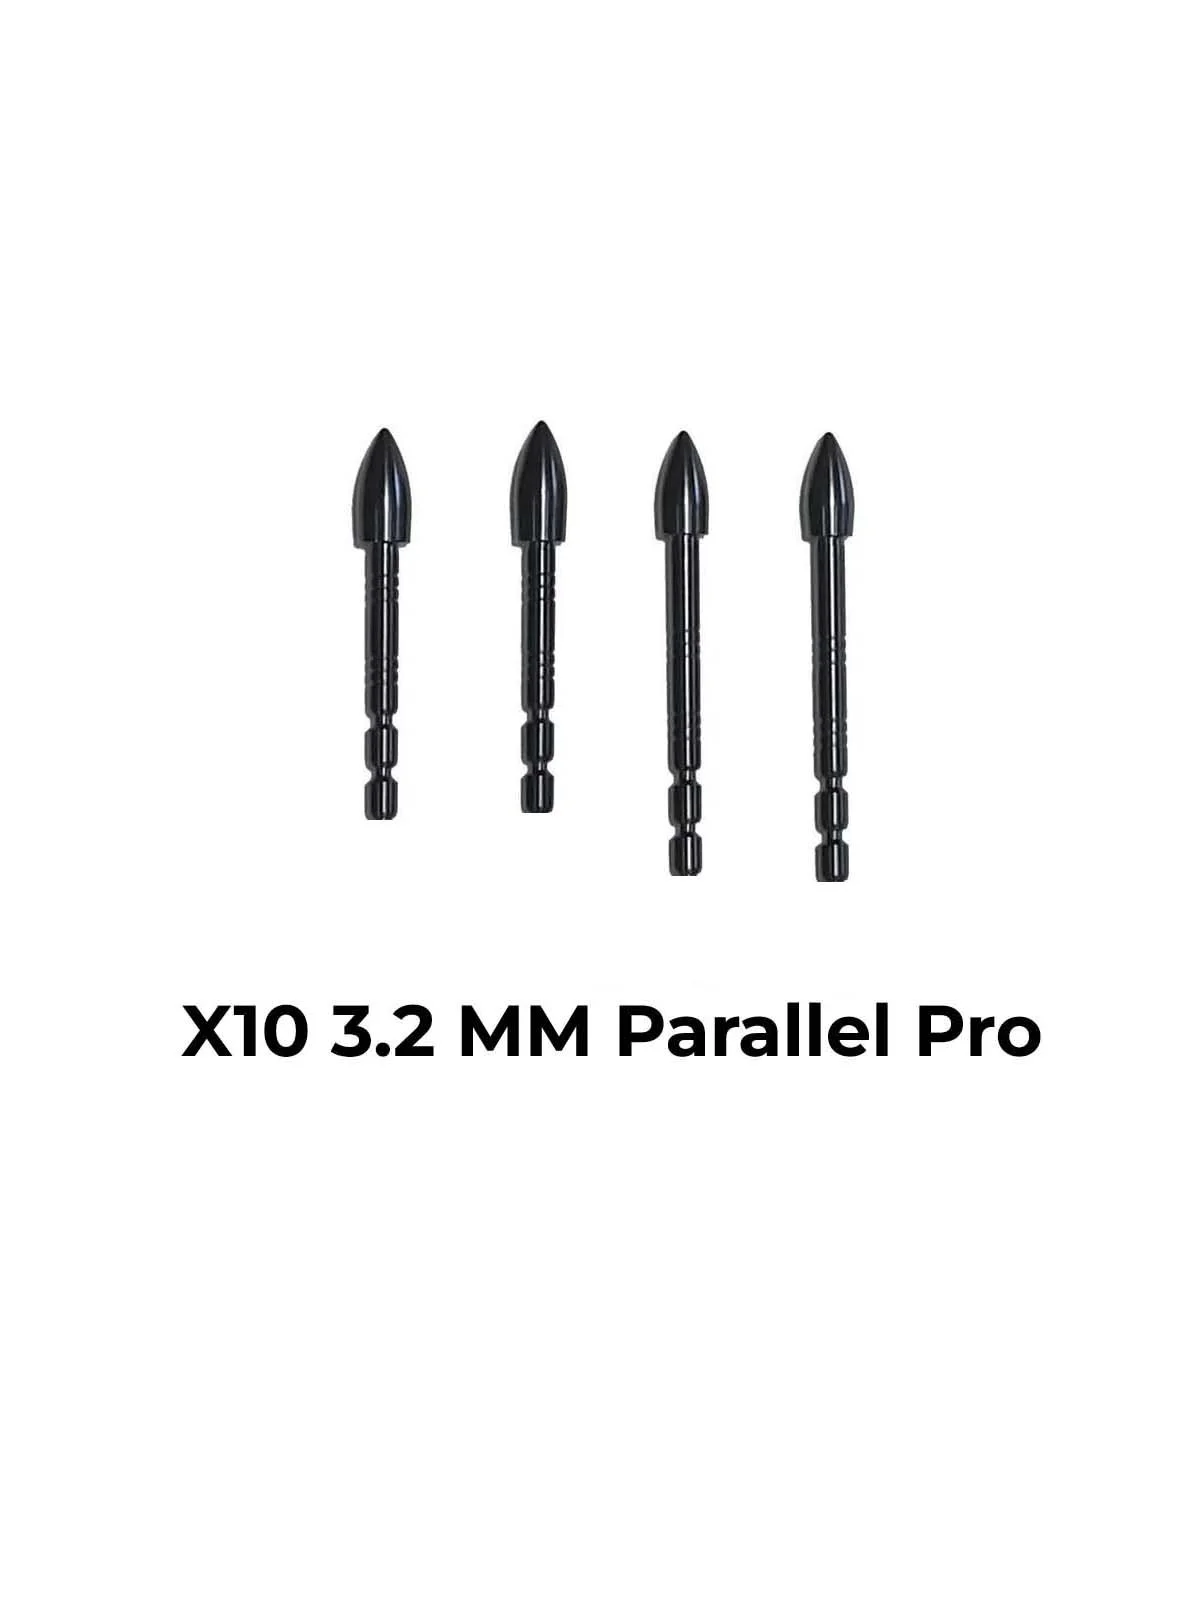
Shore Shot 97% tungsten break-off points for Easton X10 3.2 mm Parallel Pro and Black Eagle Revelation. These are not the barreled X10 / ProTour points. The shorter tungsten shank cuts how much point sits inside a parallel 3.2 mm shaft.
Points Fit - Easton X10™ 3.2 MM Parallel Pro and Black Eagle Revelation shafts
#1/D OD 0.191”
#2/C OD 0.201”
#3/B OD 0.208”
#4/A OD 0.218”
Shore Shot Archery’s Take on Tungsten Points
Easton: Available in size #1 (1000-750 Spine), #2 (700-550 Spine), #3 (500-380 Spine), and #4 (340 Spine)
Black Eagle: Available in size A (300 Spine), B (350-400 Spine), C (450-550 Spine), and D (600-800 Spine)
Each point is individually weighted and packaged
Tungsten break-off point for X10™ 3.2 MM Parallel Pro shafts
120 to 110 to 100 grains (with 2 break-offs)
Titanium plating
6 Grooves to improve glue adhesion in arrow shaft
Glue Cutout Below Head of Point For Better Adhesion In Arrow Shaft
Sold as a 12 pack
Weight tolerance: ± 0.5 grains (Matched Per Dozen ± 0.3
97% Tungsten
Shank OD .125”
*Reminder, EU customers will be responsible for paying VAT on pickup.
*Purchases outside of the United States may be subject to local taxes on delivery or additional shipping costs
Recommended Point Installation Method
(Tool Required: A butane or propane torch with small flame, pliers, cleaning materials noted below, and recommended hot melt (CDM Flitemate Hot Melt or Shop Stick)
Cut arrow shaft on high speed arrow saw and deburr the inside of shaft, removing no more then 1/4” of aluminum shaft wall
Clean the inside of the shaft (about 2” in) with 91% isopropyl alcohol
Heat hot melt in a gas flame and apply a ring of hot melt around and inside the open end of the shaft (Never Apply Heat Or Flame To The Shaft)
With your small set of pliers, grasp the point and coat the shank end of the point with hot melt that was headed by your hot flame (get hot melt soft not liquid)
Hold the point in your piers with the hot melt applied into the flame again, this time let it liquefy (MAX 3-4 Seconds Do Not Overheat the Point) Serious damage to the shaft or point could occur
Put point into shaft with a twisting motion. Quickly reheat THE POINT ONLY IF NEEDED to get in fully into the shaft. Whip excess glue with a paper towel
Stand the shaft on the point end making sure the point is completely seated in the shaft and allow it to cool before touching our shooting, DO NOT use water to cool the shaft and point